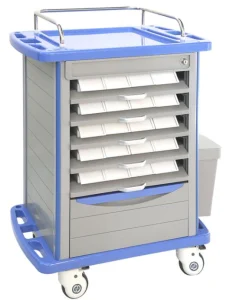
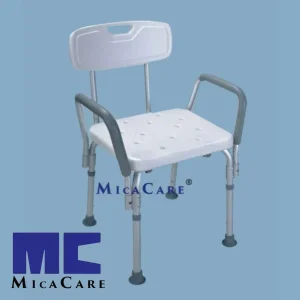
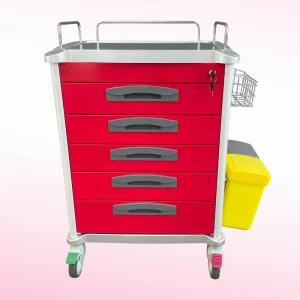
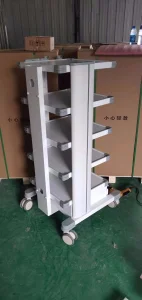
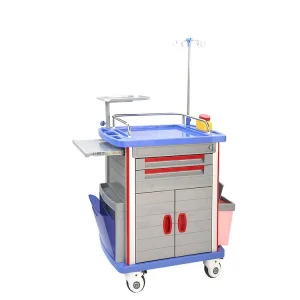
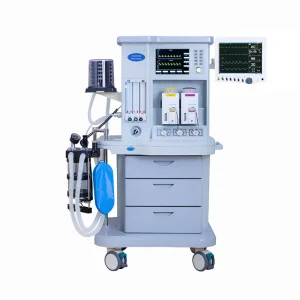
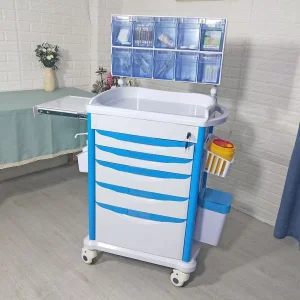
Discover our comprehensive collection of critical care carts, telemedicine mobile workstations, and patient mobility aids engineered for rigorous clinical environments worldwide.
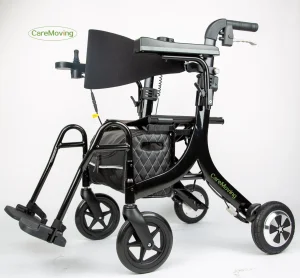
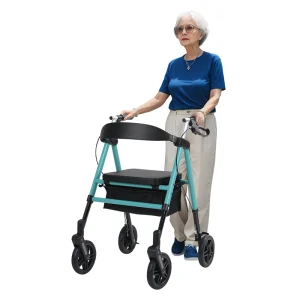
Two decades of dedicated manufacturing mastery and unwavering commitment to global clinical workflow optimization.
Shenzhen Avelar Medical Co., Ltd. was founded in 2003 and has accumulated over 21 years of rich experience in the medical technology industry. Headquartered in Pingshan, Shenzhen, with a state-of-the-art production facility in Huizhou, the company spans a total area of 10,000 square meters. As a leading national high-tech enterprise, Avelar Medical integrates cutting-edge research and development, innovative design, and high-efficiency manufacturing to deliver superior medical and healthcare solutions.
With a team of over 100 highly skilled engineers and technical professionals, and more than 200 advanced manufacturing units, Avelar Medical is committed to pushing the boundaries of technological advancements in the medical field. The company has secured more than 100 national patents, demonstrating our continuous focus on innovation.
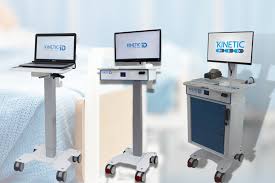
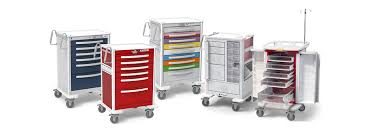
Avelar Medical specializes in a broad range of products, including medical equipment installation solutions, intelligent mobile medical devices, assistive technology for residual life support, healthcare products for the bathroom, and more. We work closely with top-tier hospitals and healthcare institutions around the world, providing them with products designed to improve patient care, enhance operational efficiency, and optimize the healthcare environment. Our solutions have reached more than 100 countries and regions, including North America, Europe, the Middle East, and Asia.
At Shenzhen Avelar Medical, our business philosophy revolves around two core principles: “Quality First” and “Customer First.” This commitment to excellence has earned us the trust of our domestic and international clients. Our innovative products, combined with exceptional service and reliable after-sales support, allow us to meet the ever-evolving needs of the global healthcare market.
As we look to the future, Avelar Medical remains dedicated to continuous growth, investment in research and development, and the creation of cutting-edge medical solutions. We are committed to improving healthcare outcomes, fostering a healthier future for communities worldwide, and making a lasting impact on the global healthcare industry.
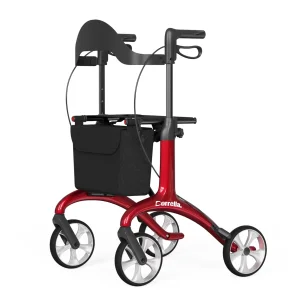
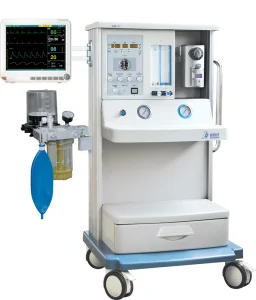
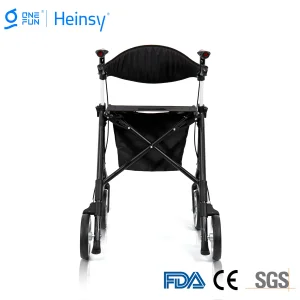
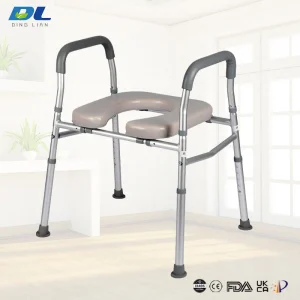
Explore our specialized surgical anesthesia workstations, ergonomic walker rollators, and secure bathroom safety solutions designed for elevated patient independence.
An authoritative analysis of modern healthcare data integration, global supply chain resilience, and the rise of smart medical manufacturing.
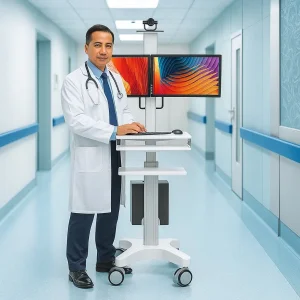
Modern healthcare systems generate immense volumes of vital sign diagnostics, telemetry records, and electronic health record (EHR) data. Seamless integration requires rugged, highly mobile hardware interfaces—such as intelligent monitor carts and dual-monitor workstations—that ensure real-time data accessibility directly at the patient bedside.
International healthcare group purchasing organizations (GPOs) and hospital distributors increasingly demand stringent regulatory compliance (ISO13485, CE, FDA standards), modular customizability, and robust OEM/ODM partnerships capable of scaling production without compromising clinical safety.
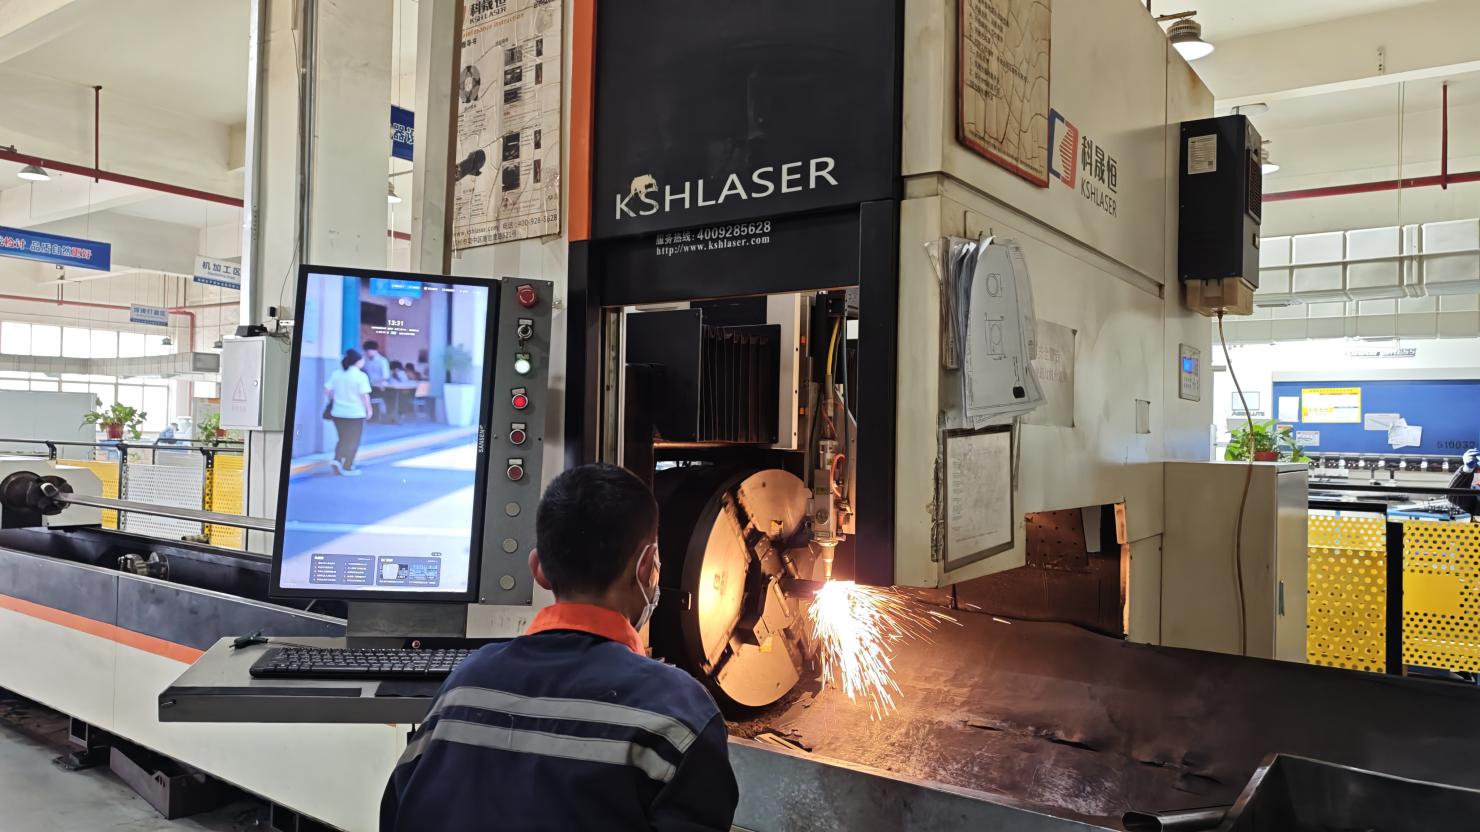
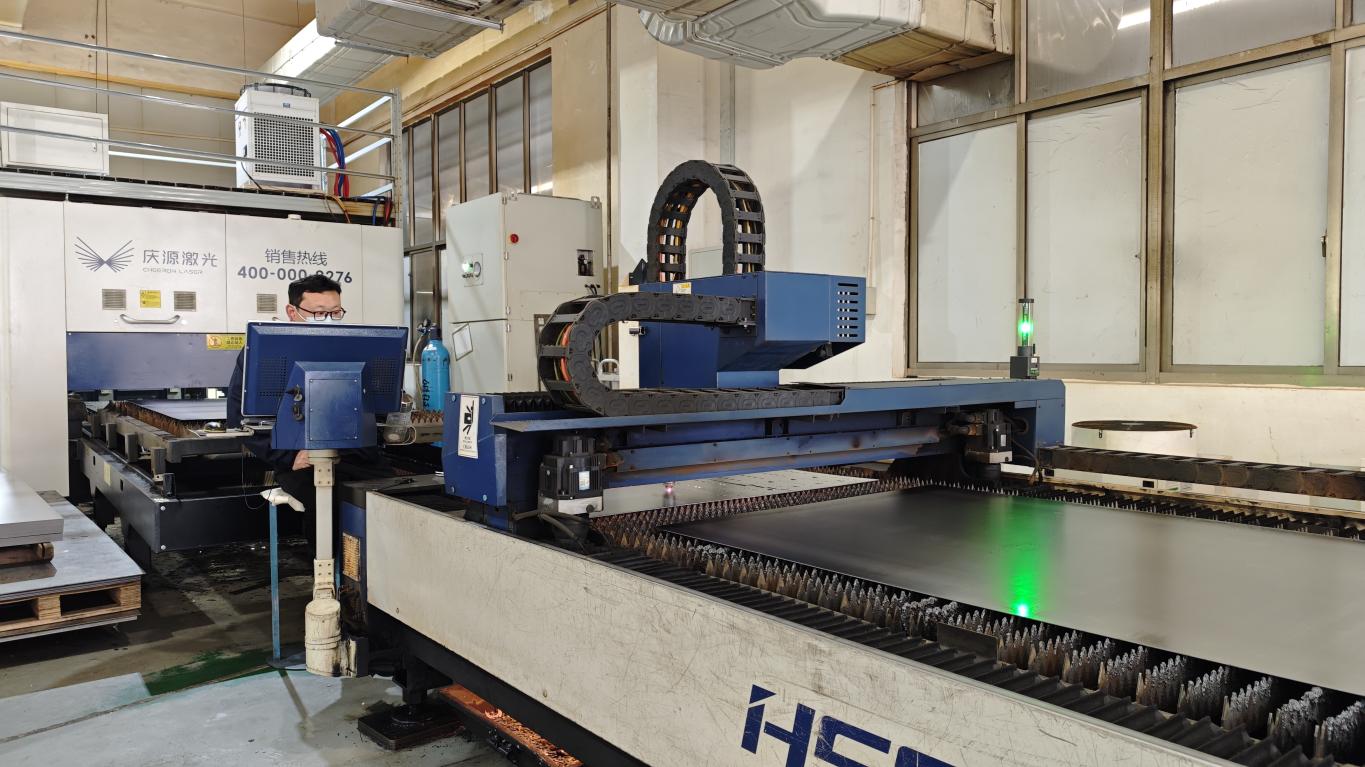
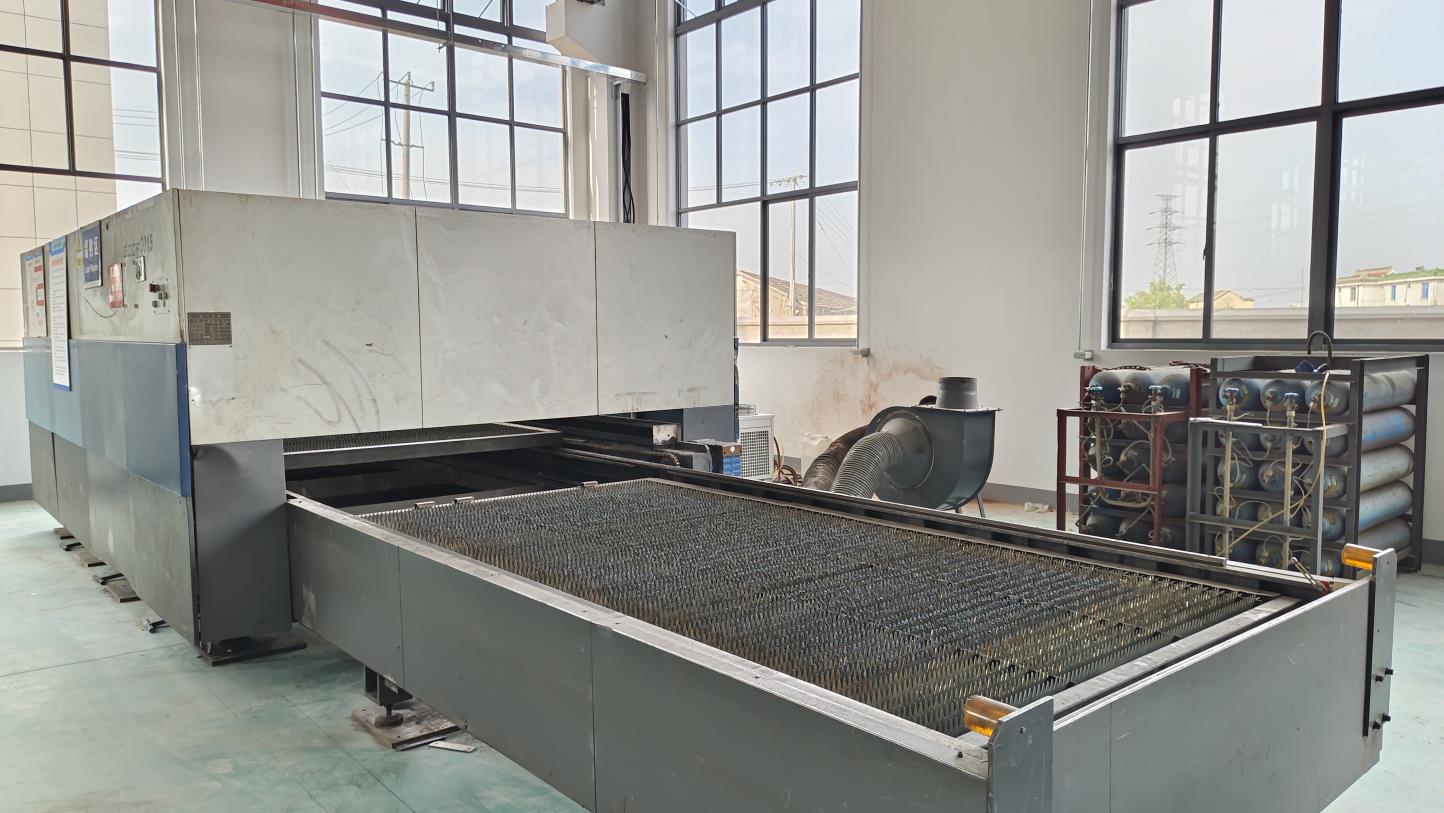
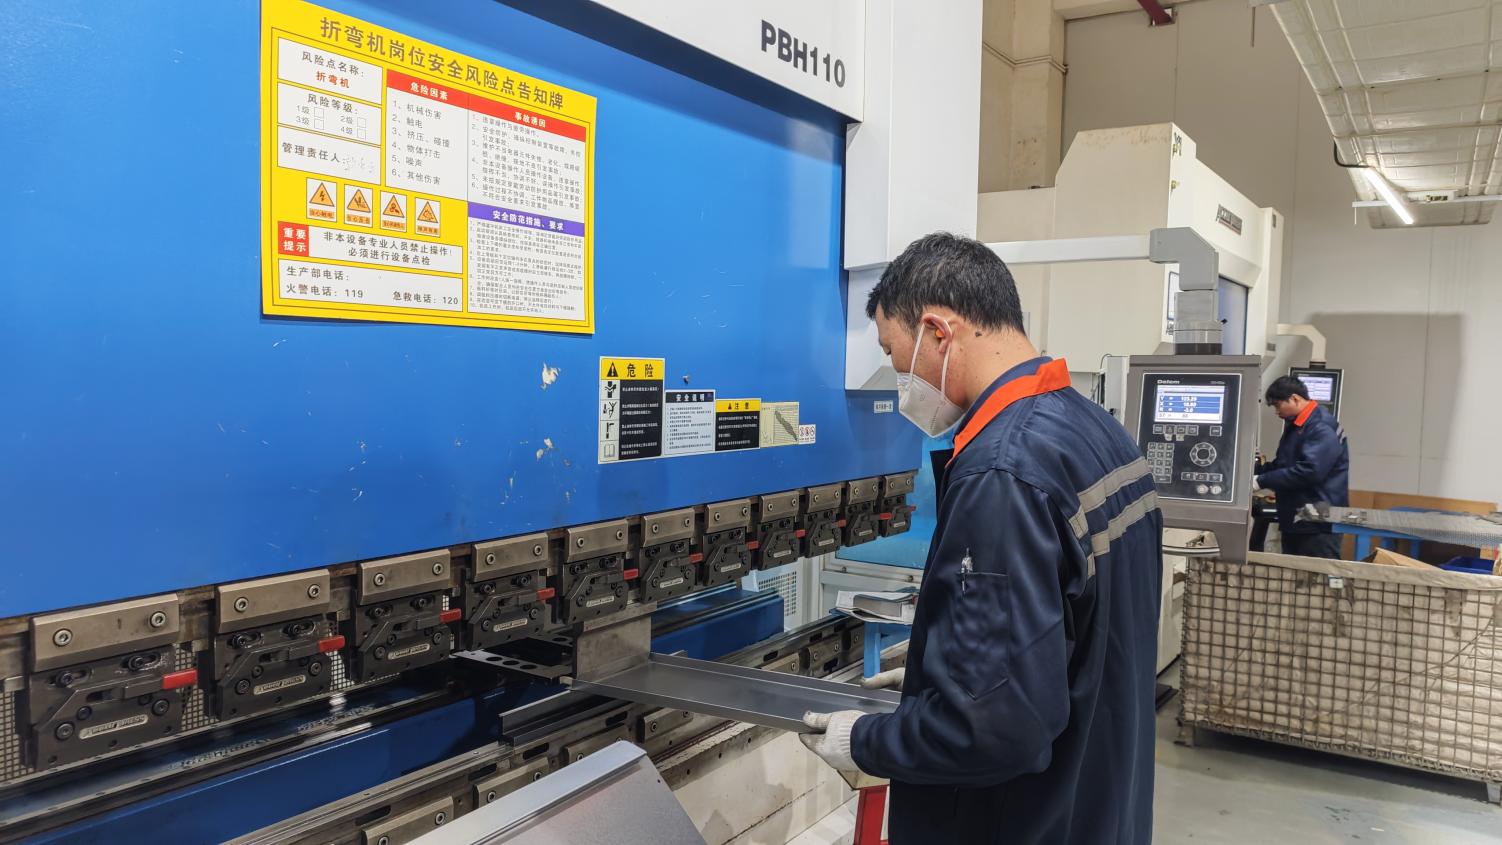
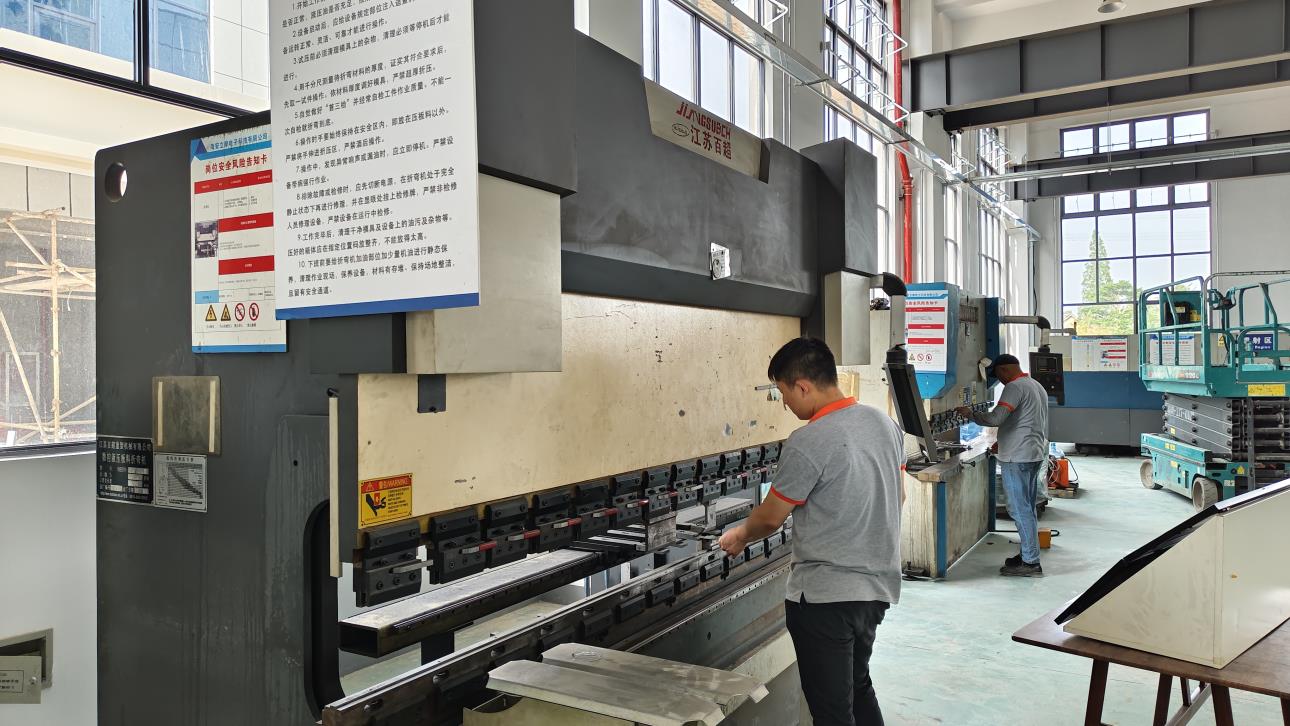
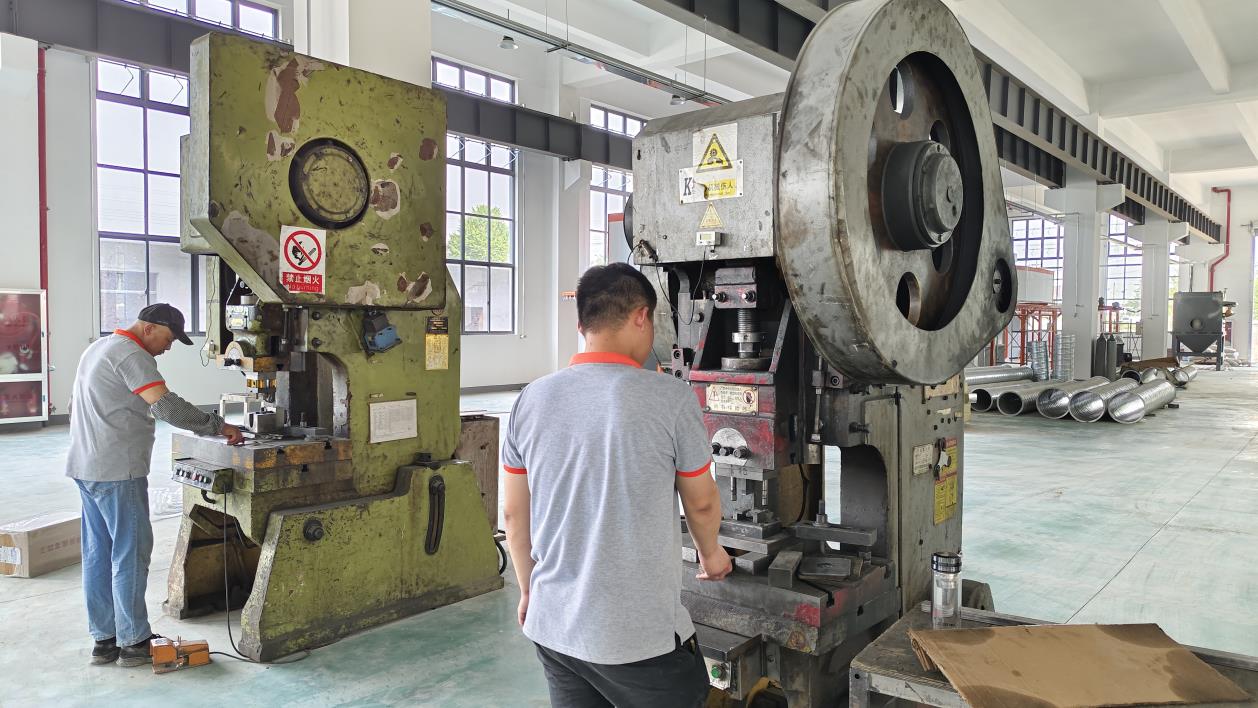
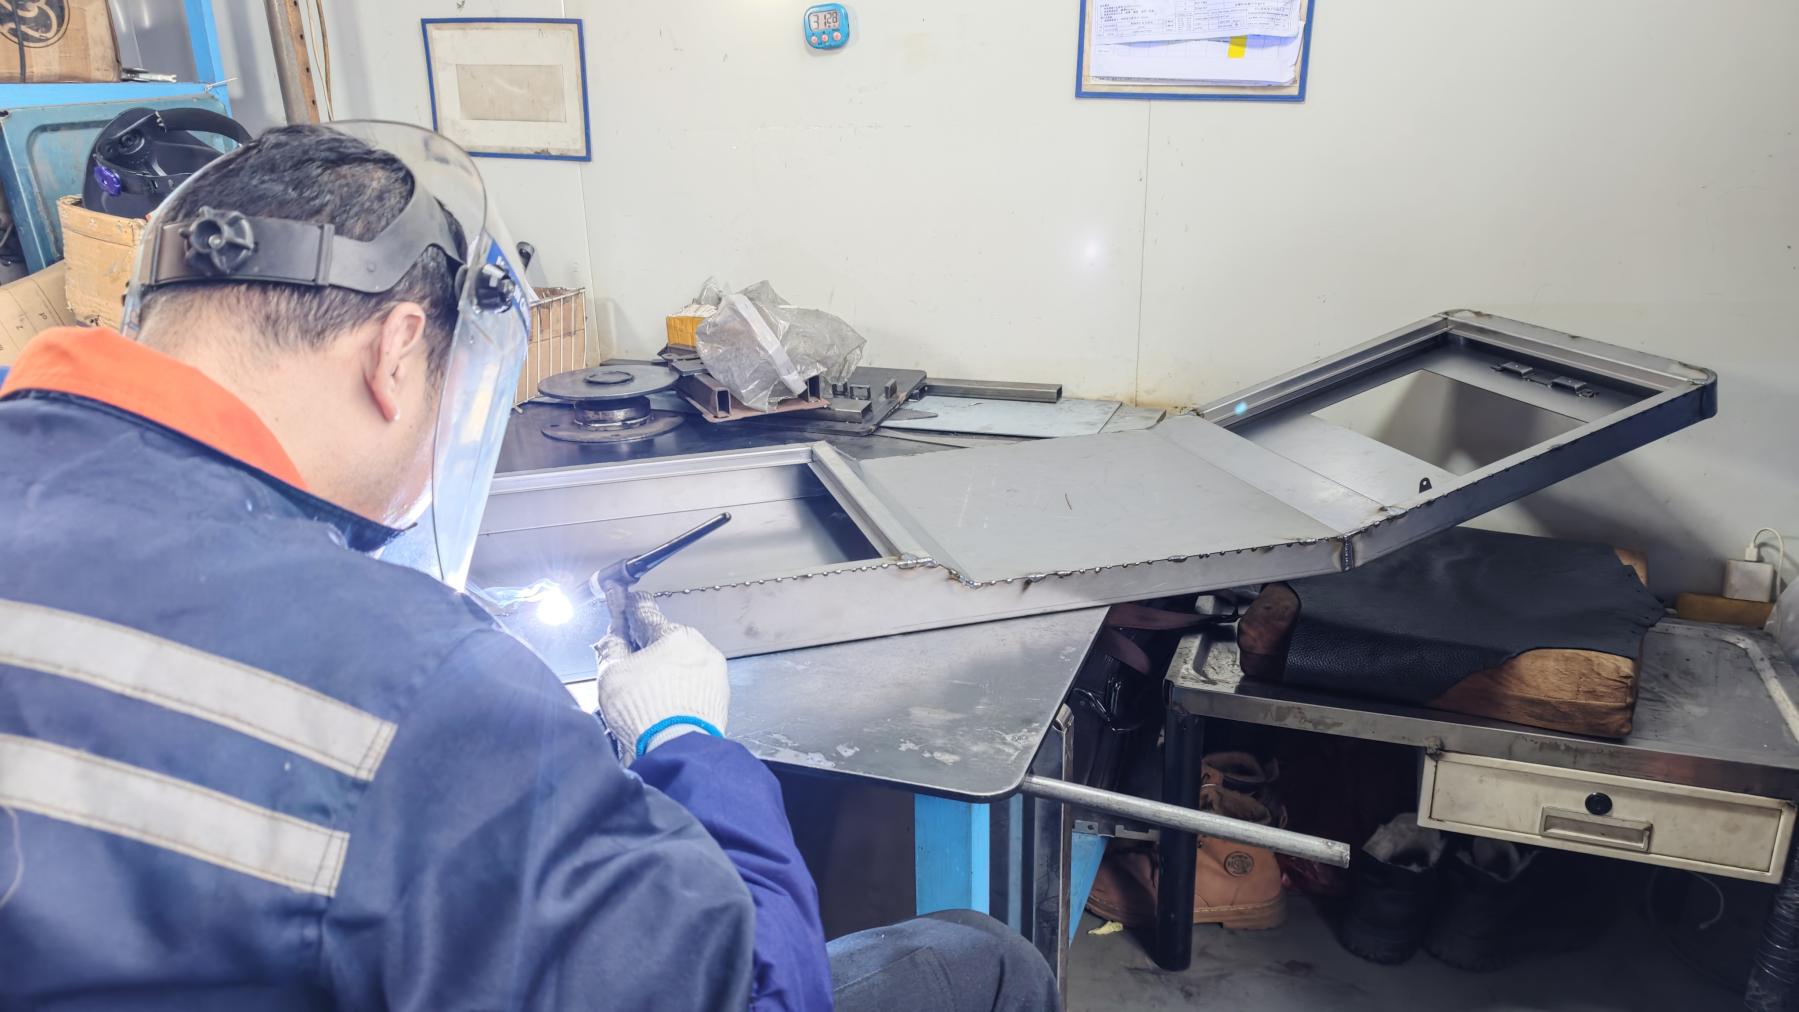
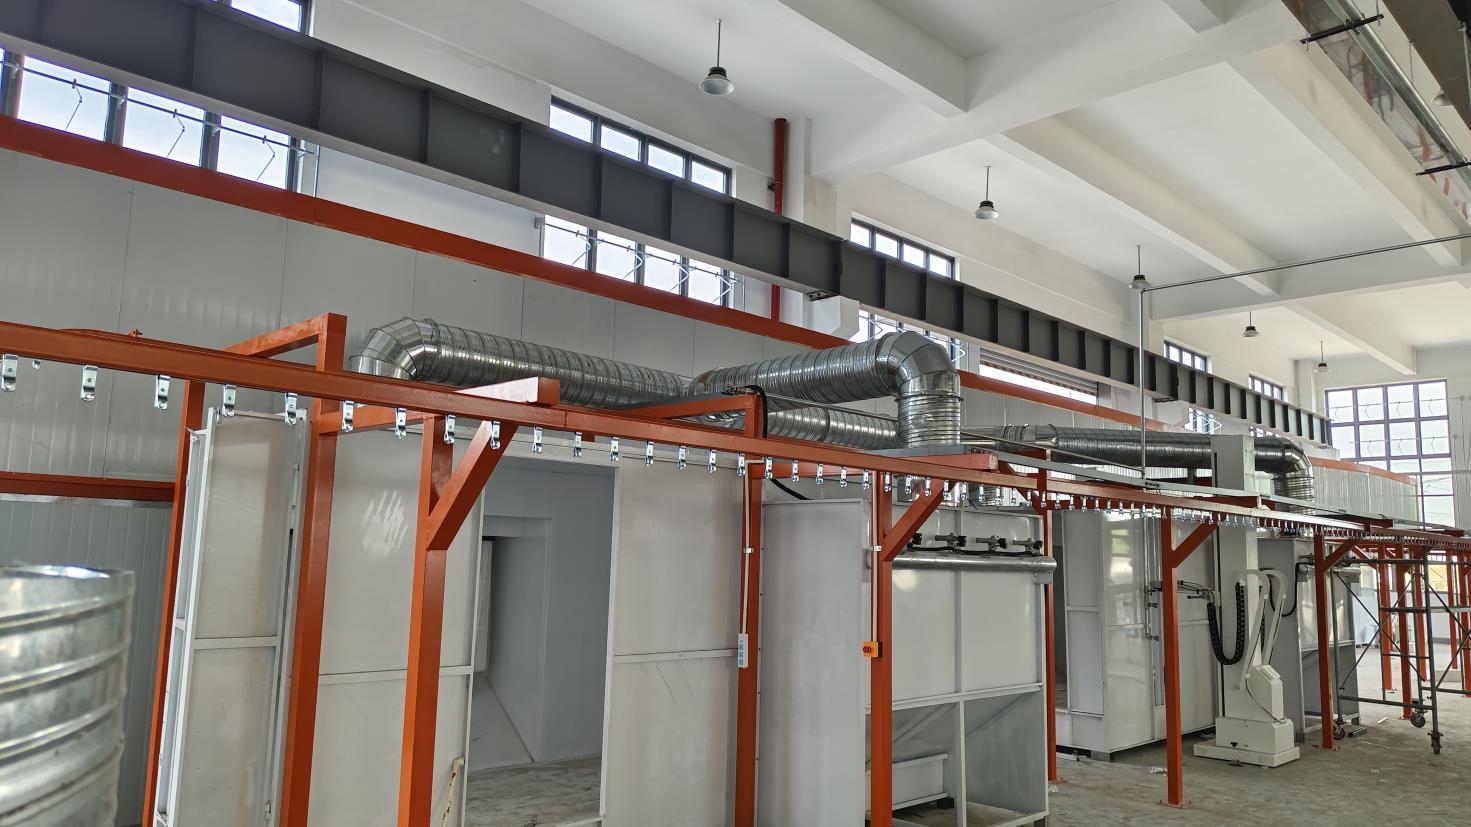
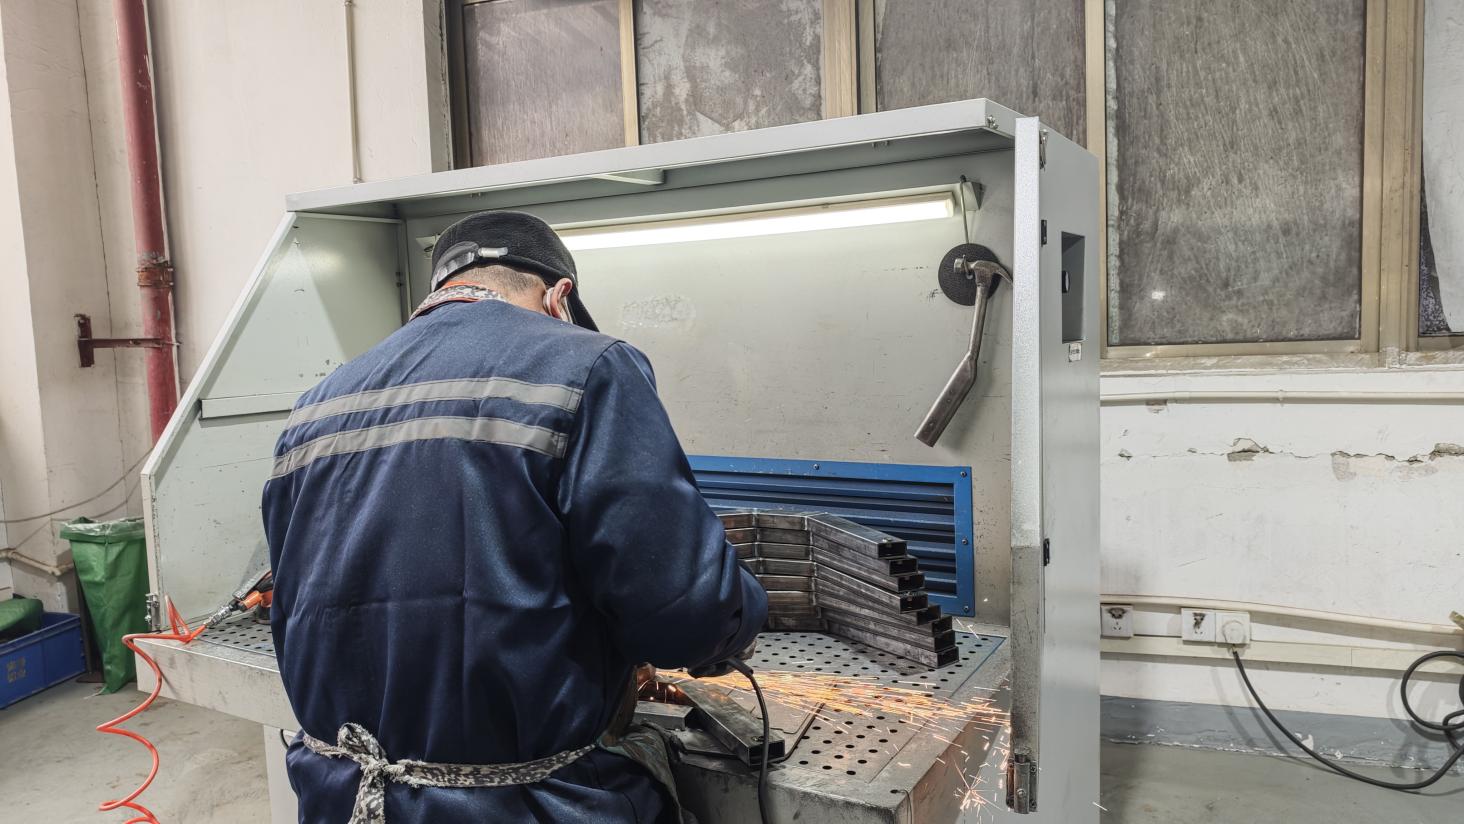
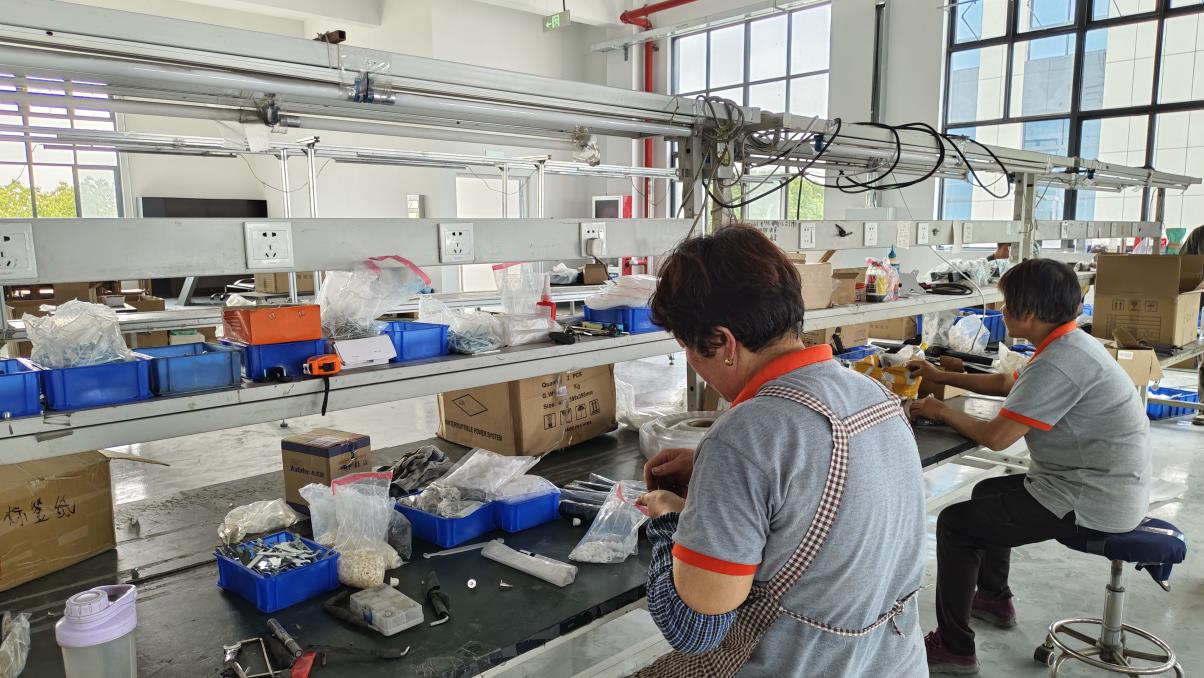
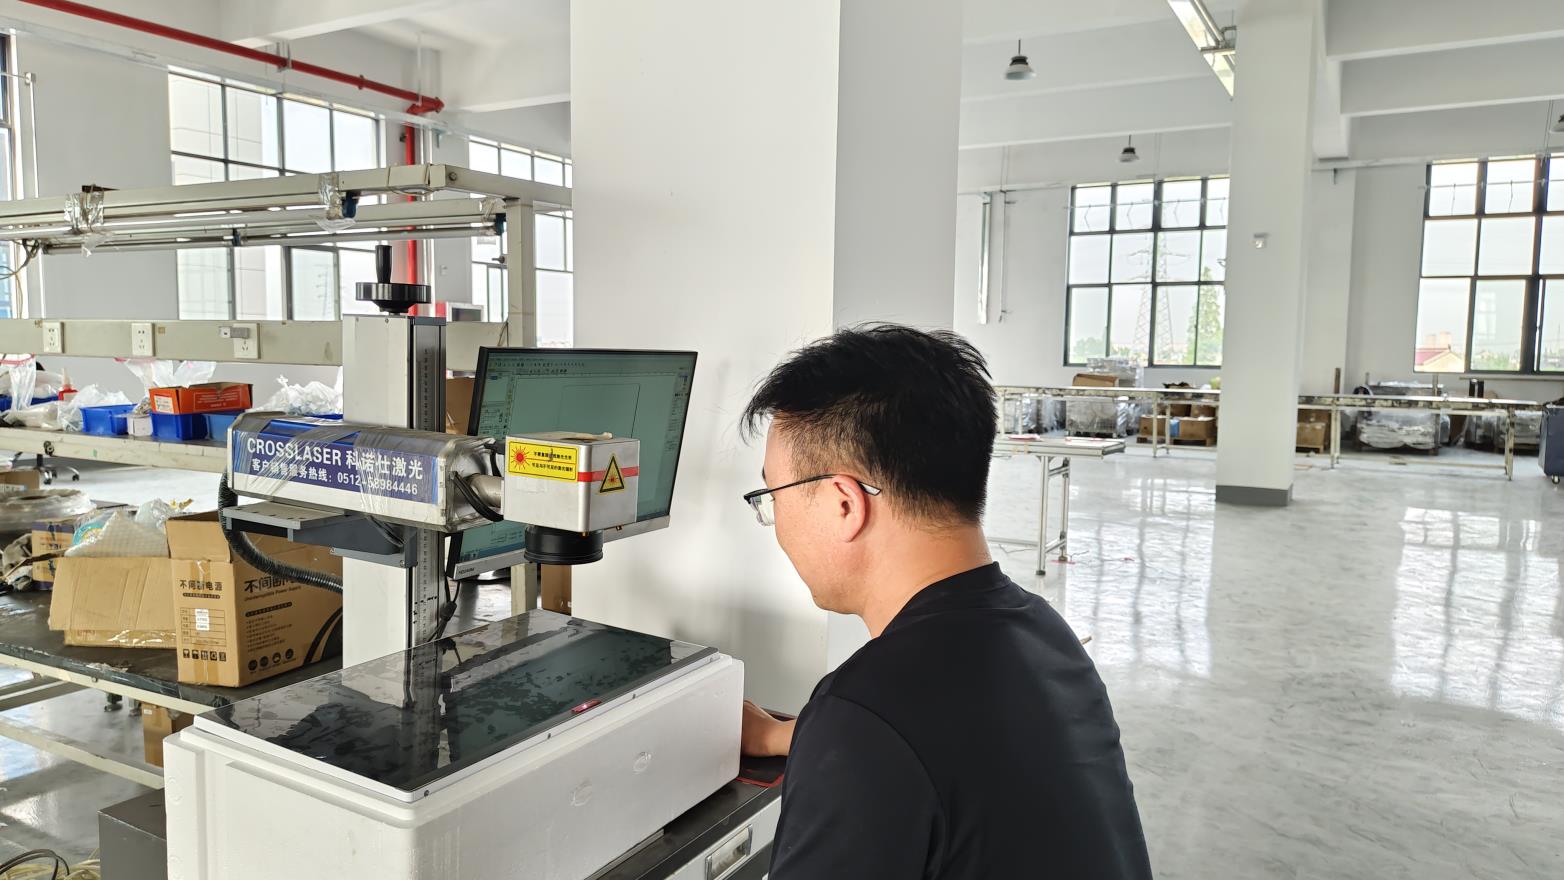
Leveraging advanced smart factories equipped with automated laser cutting, robotic welding, and precision powder coating, Chinese manufacturing excellence ensures absolute dimensional accuracy, short lead times, and unmatched cost-efficiency for global B2B buyers.
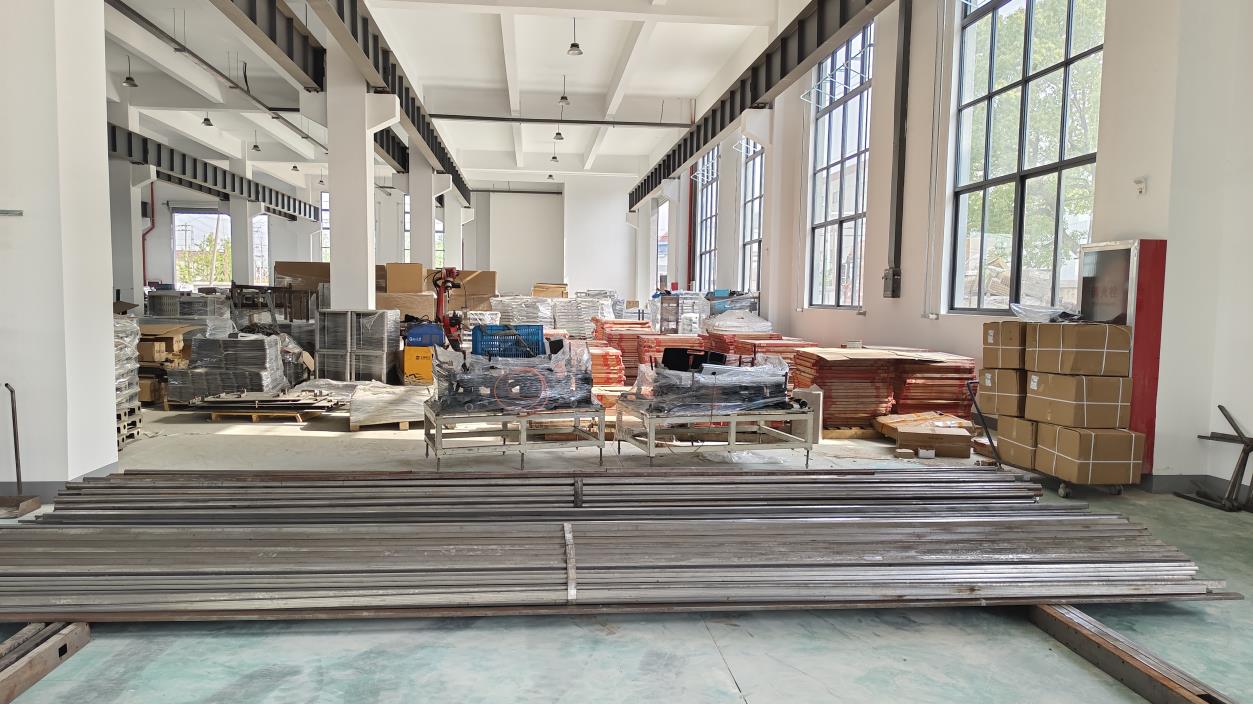
From raw metallurgical selection to pristine final packaging, explore our rigorous, vertically integrated production stages.
Expert insights addressing common procurement inquiries regarding custom OEM/ODM medical data solutions.
 Avelar Medical